How Much Capacity Does a Heat Exchanger Line Need?

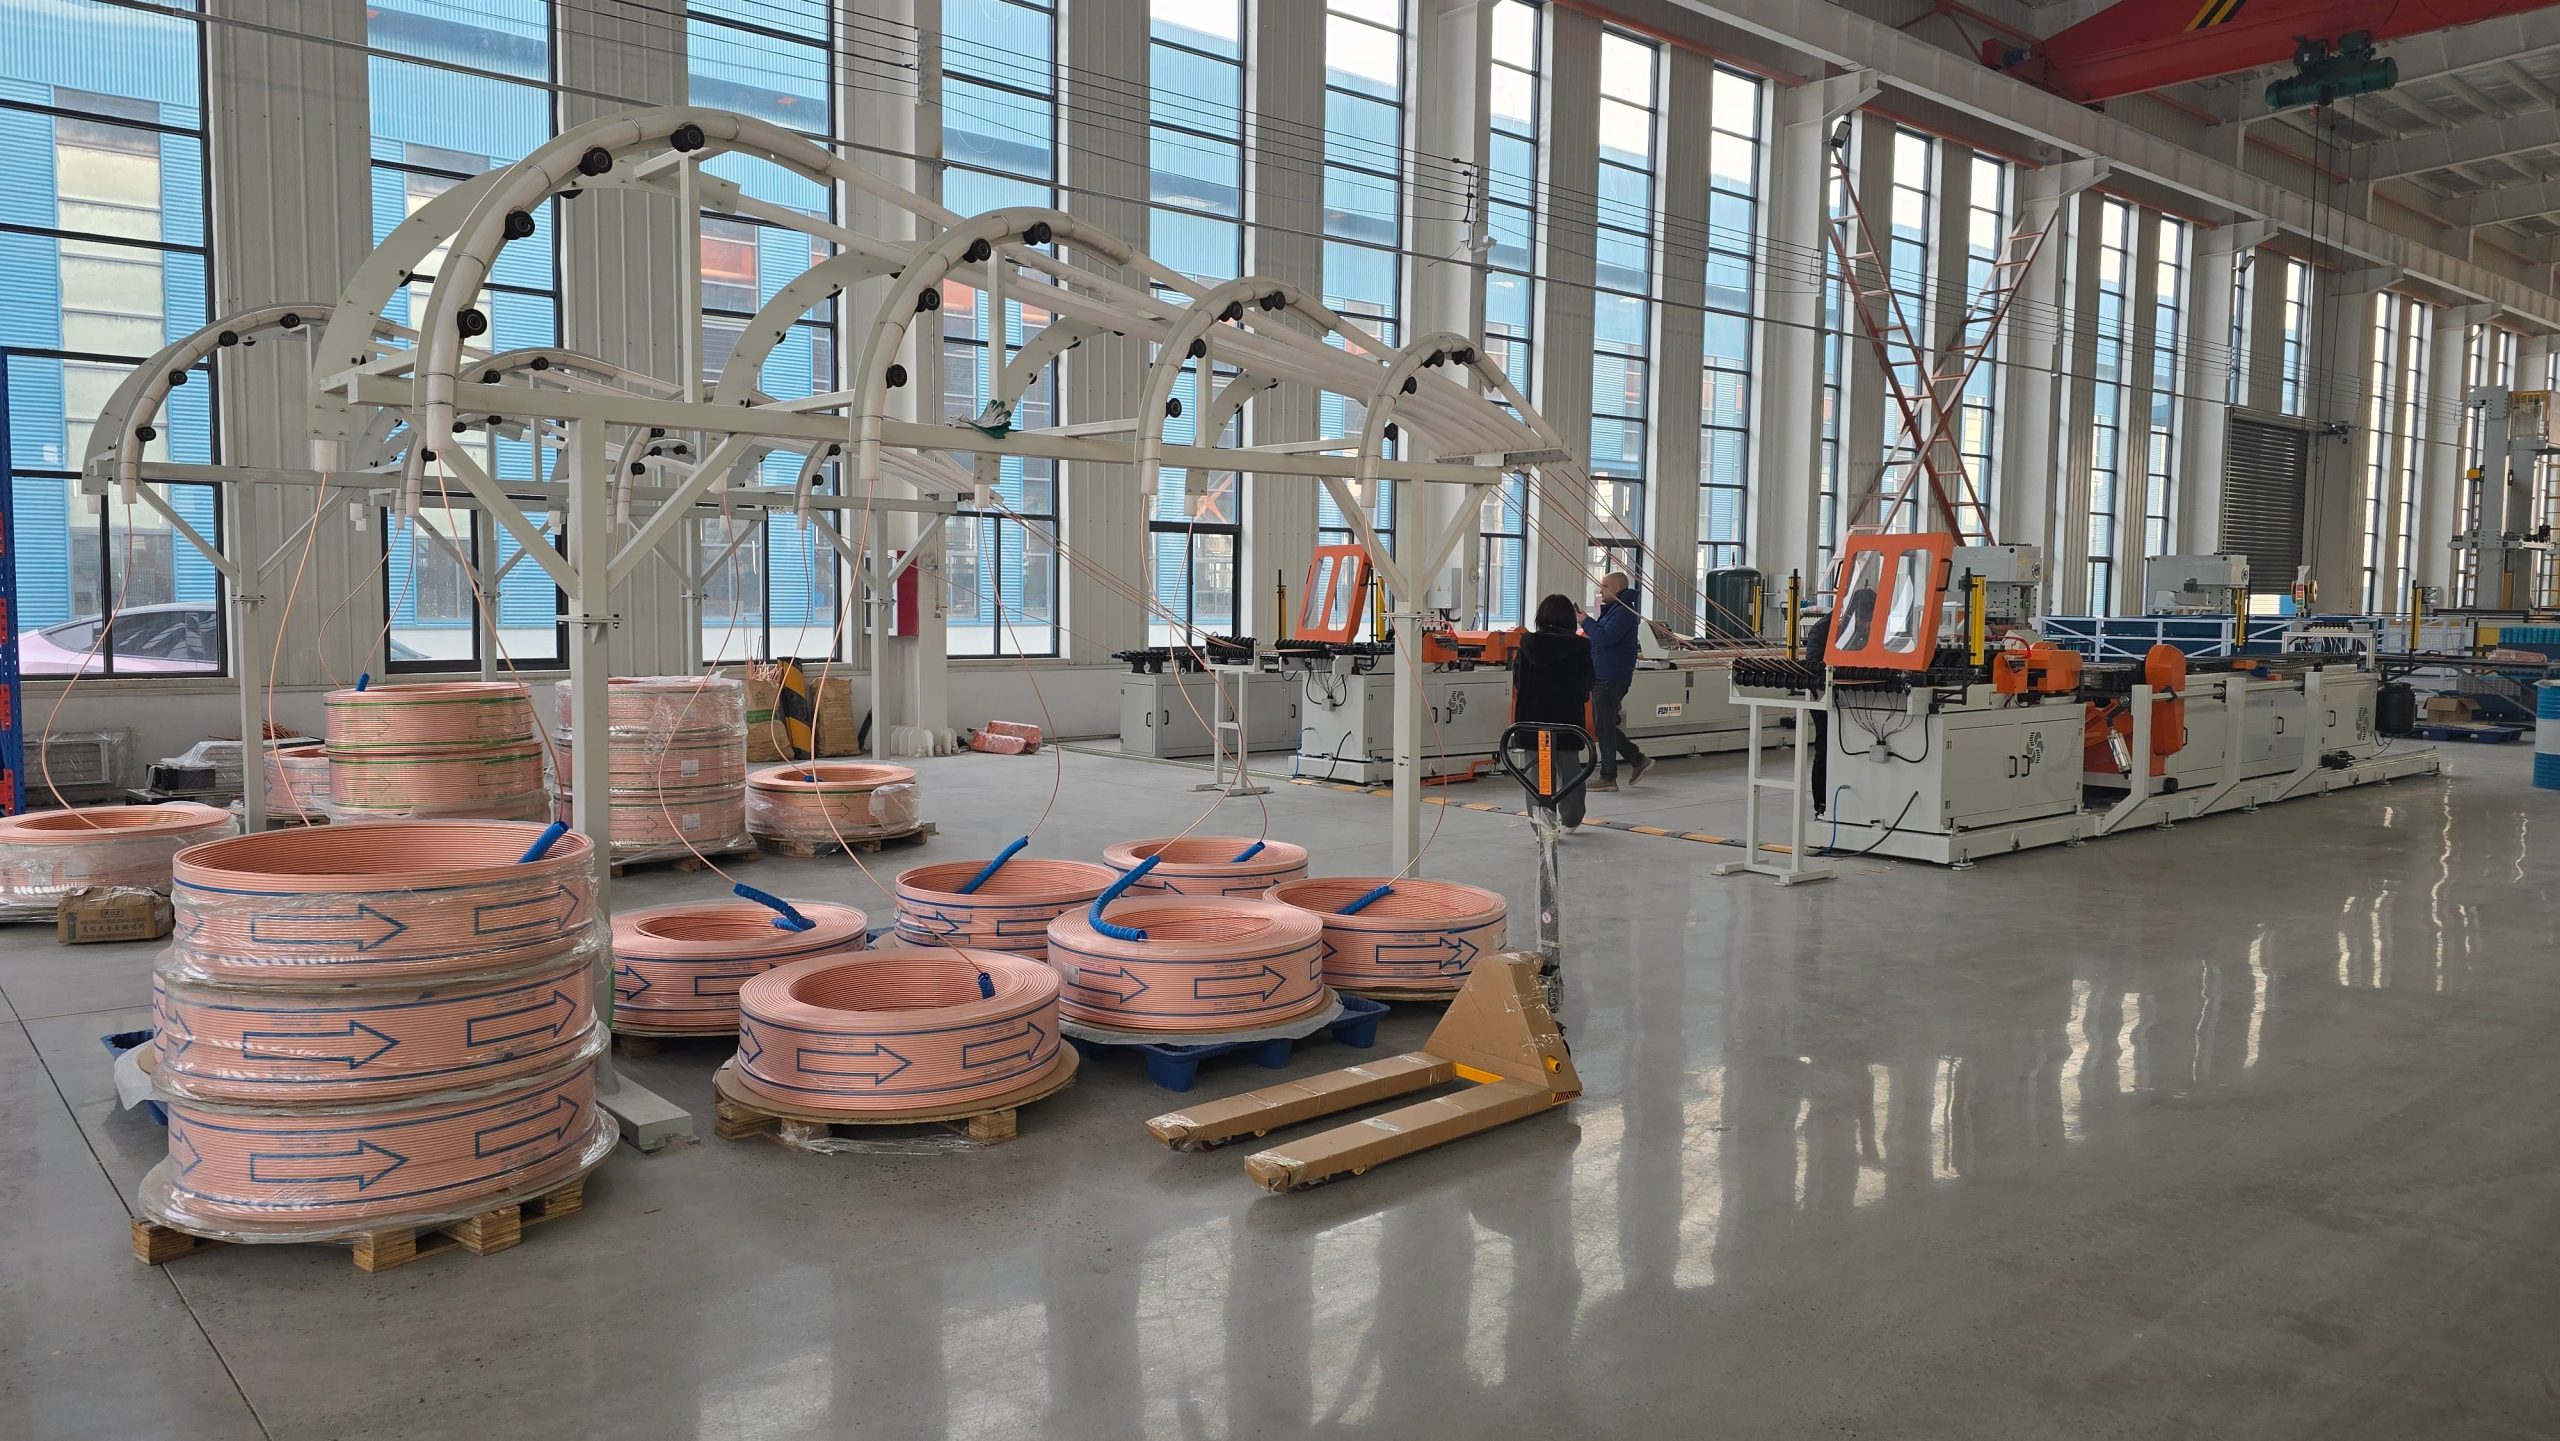
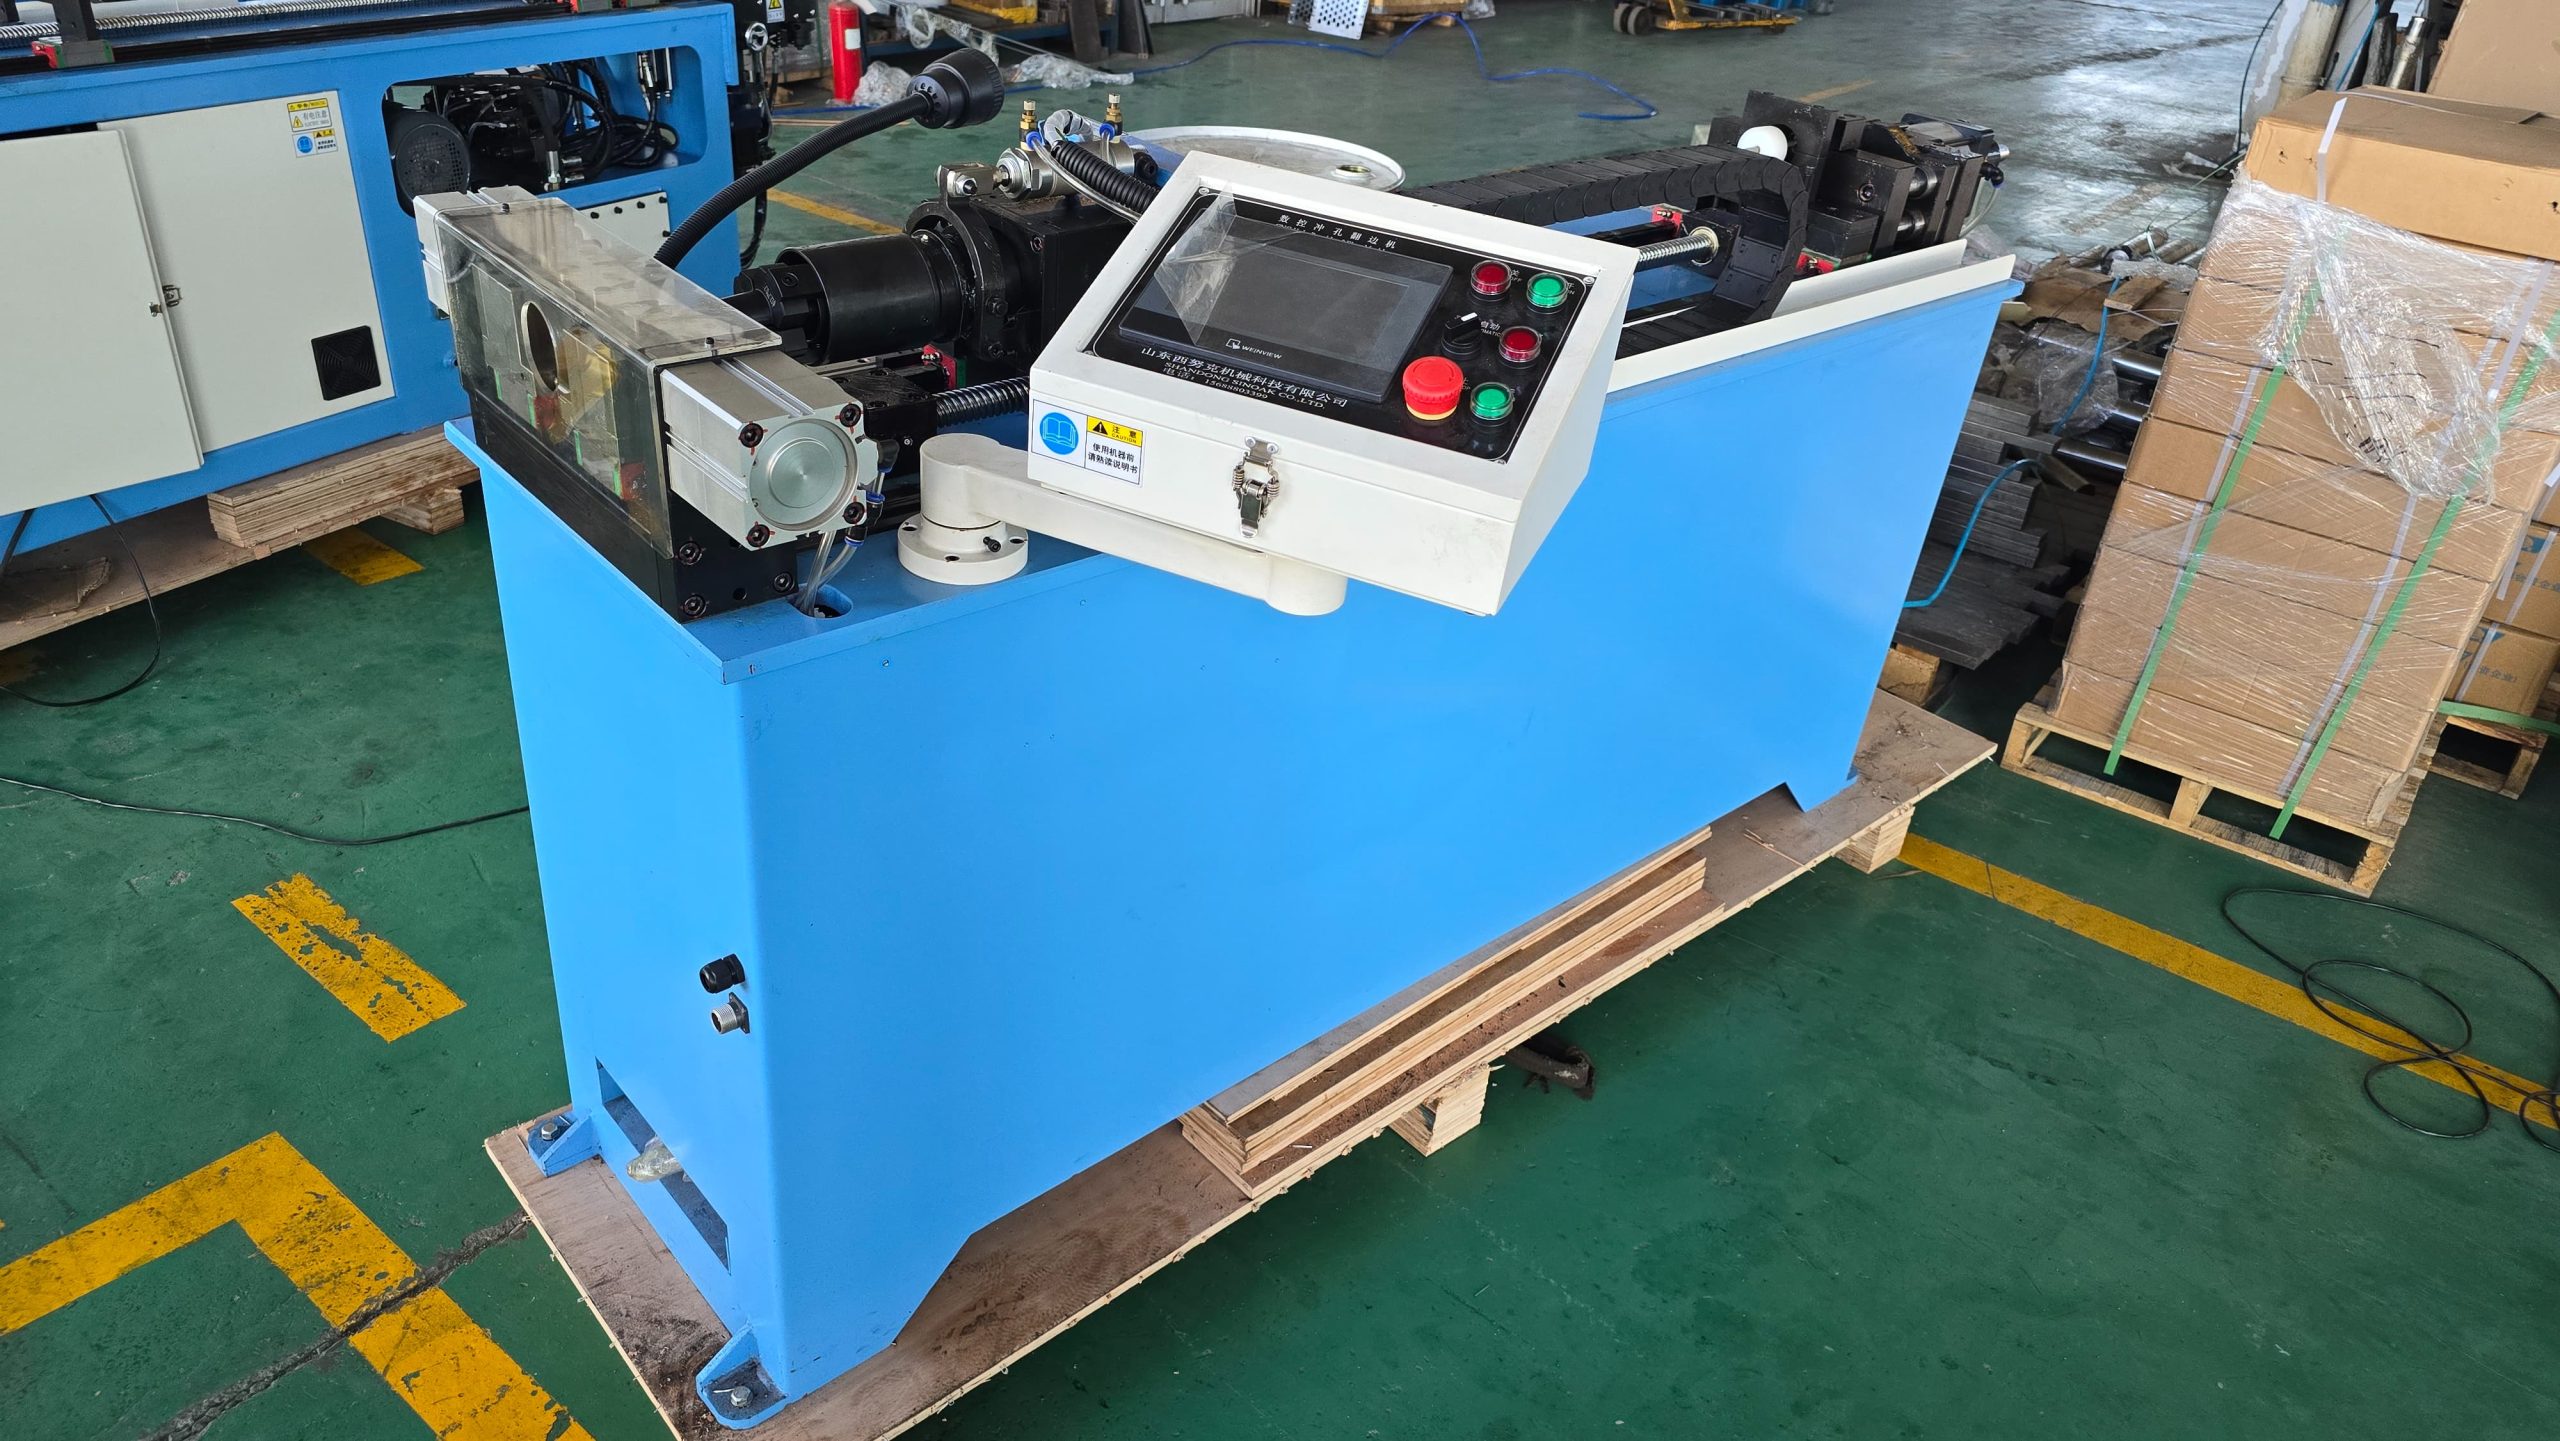
heat exchanger manufacturing automation and production equipment

How Much Capacity Does a Heat Exchanger Line Need?

Heat exchanger production capacity cannot be described reliably by finished units per hour alone. A heat exchanger production line may process coils with very different fin counts, hairpin quantities, tube circuits, brazed joints, and test times. Two products with the same daily output target can therefore create very different machine workloads.

Teams defining lean flow, bottlenecks, and improvement priorities can consult NIST MEP guidance on lean and process improvement. It does not replace a plant-specific time study, but it provides a useful framework for connecting capacity, flow, and continuous improvement.

A defensible calculation begins by converting the sales forecast into workload at each process. The planner then applies available time, changeover losses, realistic equipment performance, and first-pass yield before deciding machine quantities, automation level, and buffer size.

Heat exchanger production capacity starts with three definitions

Measure

Definition

Use in coil production

Common mistake

Takt time

Available production time divided by customer demand

Shows how often one conforming product must be completed to meet delivery demand

Including breaks, planned maintenance, or fixed changeover time as available time

Cycle time

Time required for one station to complete its work

Tests whether fin stamping, tube bending, expanding, or leak testing can support takt

Recording only machine motion and ignoring loading, inspection, or unloading

Effective capacity

Conforming output after availability, performance, and quality losses

Supports realistic equipment quantities and production planning

Using the short-term maximum machine speed as the planning rate


Takt time is demand-driven, cycle time describes station performance, and effective capacity is the output that can actually be shipped. All three must use the same time period and the same definition of a conforming product.

heat exchanger production capacity and line balancing

Convert finished-product demand into process workload

Capacity planning requires a product-family workload sheet. For each model, record the quantity of fins, hairpins, return bends, expanded tube holes, brazed joints, and test minutes required per finished coil.

Process

Recommended workload unit

Product parameters that drive workload

Fin stamping

Press strokes, fins, or strip length

Rows, die output per stroke, fin pitch, stock width, and collection method

Hairpin bending

Conforming hairpins

Cut length, tube diameter, bend radius, and number of tubes processed per cycle

Lacing and assembly

Coil cores or tubes inserted

Core dimensions, tube count, fin-hole consistency, and operator count

Tube expansion

Cores, batches, or rod strokes

Tube-hole count, core height, loading time, and rod-change time

Return bends and brazing

Bends, joints, or brazed connections

Circuit count, access, fixture design, and cleaning requirements

Pressure and leak test

Test minutes per coil

Internal volume, filling, stabilization, hold time, and evacuation


A small coil may use 12 hairpins while another model uses 48. If both require 500 finished units per shift, the bender workload is 6,000 versus 24,000 hairpins. Finished-unit demand alone is not enough for equipment selection.

A repeatable capacity calculation

  1. Define the planning period: year, month, day, or shift, including working days and shift pattern.
  2. Subtract breaks, meetings, planned maintenance, cleaning, and fixed material-change time.
  3. Convert each product-family demand into workload for every manufacturing process.
  4. Add changeover frequency, changeover duration, and first-piece approval time.
  5. Apply realistic availability, performance, and quality assumptions instead of an ideal OEE value.
  6. Calculate required machine hours for each station and compare them with available machine hours.
  7. Recheck the result for peak season, concentrated orders, and planned equipment maintenance.
  8. Reserve capacity for product changes and expansion, but do not replace calculations with an arbitrary percentage.

Use OEE without confusing nameplate speed with output

Overall equipment effectiveness separates availability, performance, and quality losses. Its purpose is to expose where output is lost, not to hide every loss inside one utilization percentage.

OEE factor

Typical loss in heat exchanger equipment

Data required

Availability

Failures, die changes, coil changes, waiting for material, cleaning, and approval

Start and finish of each stop, reason codes, and changeover frequency

Performance

Minor stops, limited loading capacity, reduced speed for quality, and slower long products

Ideal cycle, actual cycle, product specification, and operator waiting time

Quality

Fin jams, hairpin dimensional errors, expansion defects, brazing leaks, and rework

Total output, first-pass output, scrap, rework, and defect reasons


A new plant without historical data should define separate conservative assumptions for each station and replace them after stable trial production. A fin press with frequent die changes and a leak tester with fixed stabilization time should not automatically receive the same OEE assumption.

Find the true bottleneck under the product mix

The bottleneck is the resource that limits shipment under the current product mix and schedule. It can move: long hairpins may constrain bending, high tube-hole counts may move the constraint to expansion, and high-pressure products may be limited by test hold time.

  • Multiply station time by demand for each product family to calculate the mixed-product load.
  • Study busy periods rather than shift averages, including loading, inspection, and material handling.
  • Improve bottleneck changeover, minor stops, and first-pass yield before purchasing another machine.
  • Do not force non-bottleneck stations to run continuously when the result is only more work in process.
heat exchanger production capacity and line balancing

Size buffers by recovery time and product risk

Buffers should isolate short disturbances, not conceal permanent imbalance. A practical starting point is the common recovery time of the upstream process multiplied by the bottleneck consumption rate. The buffer also needs a maximum limit that triggers speed reduction or a controlled stop.

Fin stacks, long hairpins, and expanded cores cannot use the same storage rule. Fins need protection against crushing and model mixing; long tubes need continuous support; assembled cores need controlled orientation and safe handling. Buffer size must therefore satisfy both flow and quality requirements.

Common quality problems when capacity is overstated

Problem

Likely cause

Adjustment

Capacity correction

Fin-hole variation, misfeed, or die jams

Press speed exceeds the stable material and die window; lubrication is inconsistent

Validate continuous speed by material and pitch; control die maintenance and lubrication

Use sustained conforming speed, not a short peak

Hairpin length drift, ovality, or scratches

Feed slip, unstable lubrication, or unloading cannot keep pace

Time feeding, bending, unloading, and handling separately; improve tube support

Include reduced speed, scrap, and handling loss

Under-expansion, over-expansion, or core distortion

Critical positioning, clamping, or hold time is shortened to chase output

Set force, stroke, and action time from the qualified process; optimize loading separately

Use the complete conforming cycle

False leak-test rejects or insufficient hold time

Filling, stabilization, or hold time is shortened; connectors are worn

Define the test cycle from internal volume and the test standard; maintain connectors

Include retest, false reject, and connector-change time

Data to provide before equipment selection

  1. Annual, monthly, and shift demand for every product family, including peak-season demand.
  2. Fins, hairpins, return bends, tube holes, brazed joints, and test time per product.
  3. Boundary drawings covering minimum and maximum tube diameters, lengths, and core sizes.
  4. Shift schedule, breaks, planned maintenance, cleaning, and handover arrangements.
  5. Changeover frequency, tooling range, and target changeover time.
  6. Actual OEE, stop structure, first-pass yield, and rework data, or the source of assumptions for a new plant.
  7. Operator plan, automatic loading scope, material-handling method, and available buffer space.
  8. Acceptance product mix, continuous run time, conforming-output definition, and permitted stops.

FAQ

How much spare capacity should a heat exchanger line have?

There is no universal percentage. Demand uncertainty, seasonal peaks, changeovers, maintenance, and expansion lead time should be evaluated separately. Capacity that is difficult to add quickly deserves the clearest reserve.

Why is fin press maximum speed not the available capacity?

Maximum speed normally describes short operation under defined material, die, and collection conditions. Real output also includes coil changes, lubrication, die care, jams, inspection, and first-pass yield.

Does more automation always increase effective capacity?

No. Automation can reduce loading variation, but it also increases dependence between stations. With frequent product changes or slow fault recovery, linked-line downtime can offset the cycle-time benefit.

How should a new plant estimate OEE?

Create separate availability, performance, and quality assumptions for each station under conservative, base, and improved scenarios. Replace the assumptions with actual stop, cycle, and quality data after trial production.

Conclusion

Capacity should be calculated from required shipments, converted into fins, hairpins, expanded holes, brazed joints, and test minutes. Real available time, OEE, changeovers, and first-pass yield then determine the bottleneck, machine quantity, and buffer. The maximum speed of one machine is only an input, never the final production capacity.

Leave a Reply

Your email address will not be published. Required fields are marked *