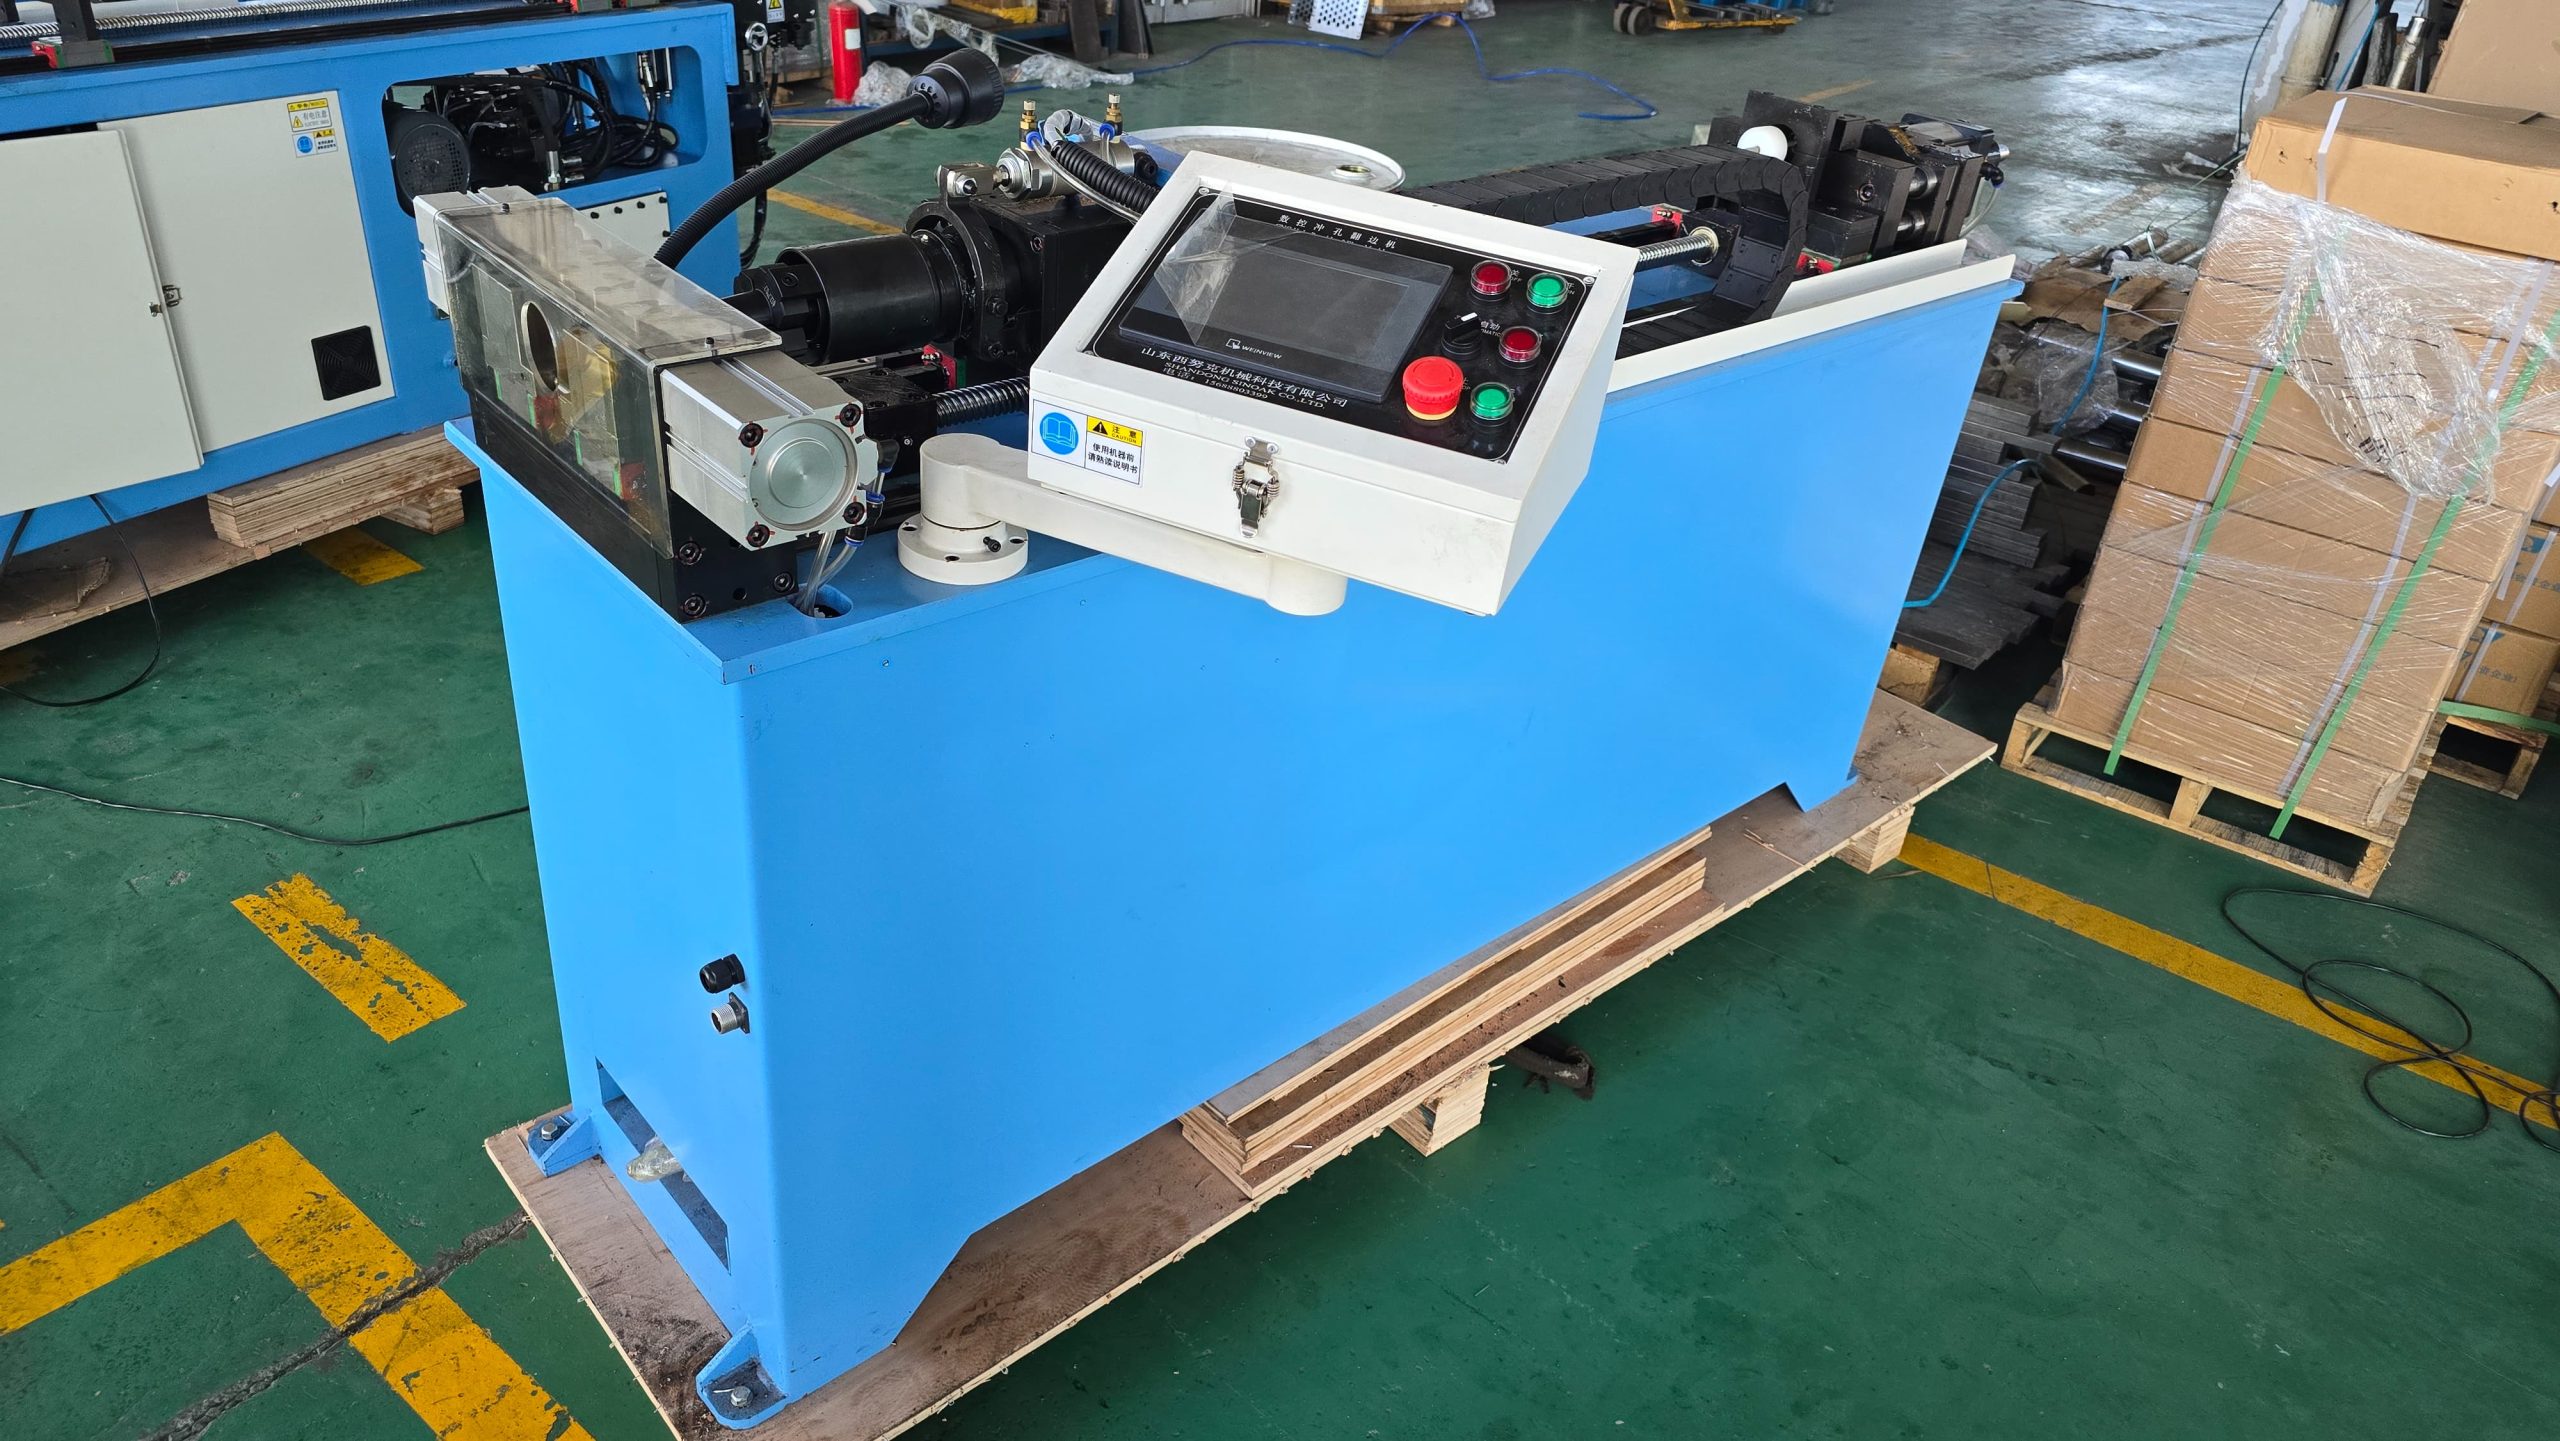
Automatic or Semi Automatic Hairpin Bender Machine
Steve
2026-09-18
Automatic or Semi Automatic Hairpin Bender Machine
hairpin bender machine selection should begin with the full tube route, not only the bend time. Automatic and semi-automatic systems can both form reliable U-bends for heat exchanger coils, but the better option depends on whether the tube arrives as coil or straight tube, how often products change, where labor is spent and how the hairpins flow to tube insertion.
Where repeated loading, carrying and unloading are major parts of the work, the OSHA ergonomics guidance can help a factory identify tasks that deserve a structured handling and safeguarding review before automation is specified.
A hairpin is more than a bent copper tube. Tube length, end flatness, bend radius, ovality, surface condition, springback and unloading direction all influence tube insertion, expansion and later brazing or assembly. The equipment choice must therefore protect the whole tube-to-coil process window.
Hairpin Bender Machine Automatic and Semi Automatic Options
|
Selection factor |
Automatic hairpin bender |
Semi-automatic hairpin bender |
Decision implication |
|
Tube route |
Can combine coil pay-off, straightening, length control, cutting, bending and unloading in a continuous sequence. |
Usually needs manual tube loading, positioning or assisted transfer before bending and unloading. |
Continuous coil processing reduces transfers and re-loading; its value is not only bend speed. |
|
Product flexibility |
Best suited to stable product families with defined tube sizes, lengths and bend forms. |
Often easier to adapt for frequent trials, short runs and wider product variation. |
When product changes are frequent, examine setup, guides, programs and tooling before prioritizing automation level. |
|
Labor and handling |
Can reduce manual pick-up, loading, transfer after straightening and placement of finished hairpins. |
Operators still manage loading, first-piece checks, collection or batch changes. |
Separate labor into processing, carrying, waiting, inspection and changeover before calculating automation benefit. |
|
Factory requirements |
Needs stable coil supply, safeguarding, material buffer, service access and a defined recovery method for faults. |
Places fewer constraints on material interfaces, but needs clear operating standards and long-tube support. |
Higher automation requires more planning for material flow, work-in-progress and abnormal recovery. |
|
Investment approach |
Higher initial integration demand can be justified by stable output and reduced handling across a defined product family. |
A practical way to start with variable demand or new products while preserving direct operator control. |
Compare sustained qualified output and flexibility, not only machine cost or stated cycle time. |
Automatic and semi-automatic machines are not simply higher and lower grades of equipment. A flexible semi-automatic machine may be the stronger choice for a mixed product program. An automatic system becomes more valuable when tube routing is stable, manual transfer is a clear bottleneck and the factory can maintain a controlled continuous process.

Map the Tube Route Before Choosing Equipment
The project team should first decide whether copper tube enters as coil and is processed directly into a hairpin, or whether it is straightened and cut at one station before being loaded into a separate bender. This decision affects material traceability, length consistency, labor, intermediate storage and the balance between tube preparation and coil assembly.
|
Tube route |
Main benefit |
Control points that must be defined |
|
Coil to hairpin in one flow |
Reduces storage, carrying and secondary loading of straight tubes; supports continuous production for stable parts. |
Coil quality, feed, straightening, length control, springback, unloading and recovery must be proven together. |
|
Straighten and cut before bending |
Supports flexible scheduling after straight-tube preparation and can suit trials or smaller batches. |
Straight-tube storage, loading, turning and transport can add scratches, mixed lengths, loading errors and manual-cycle variation. |
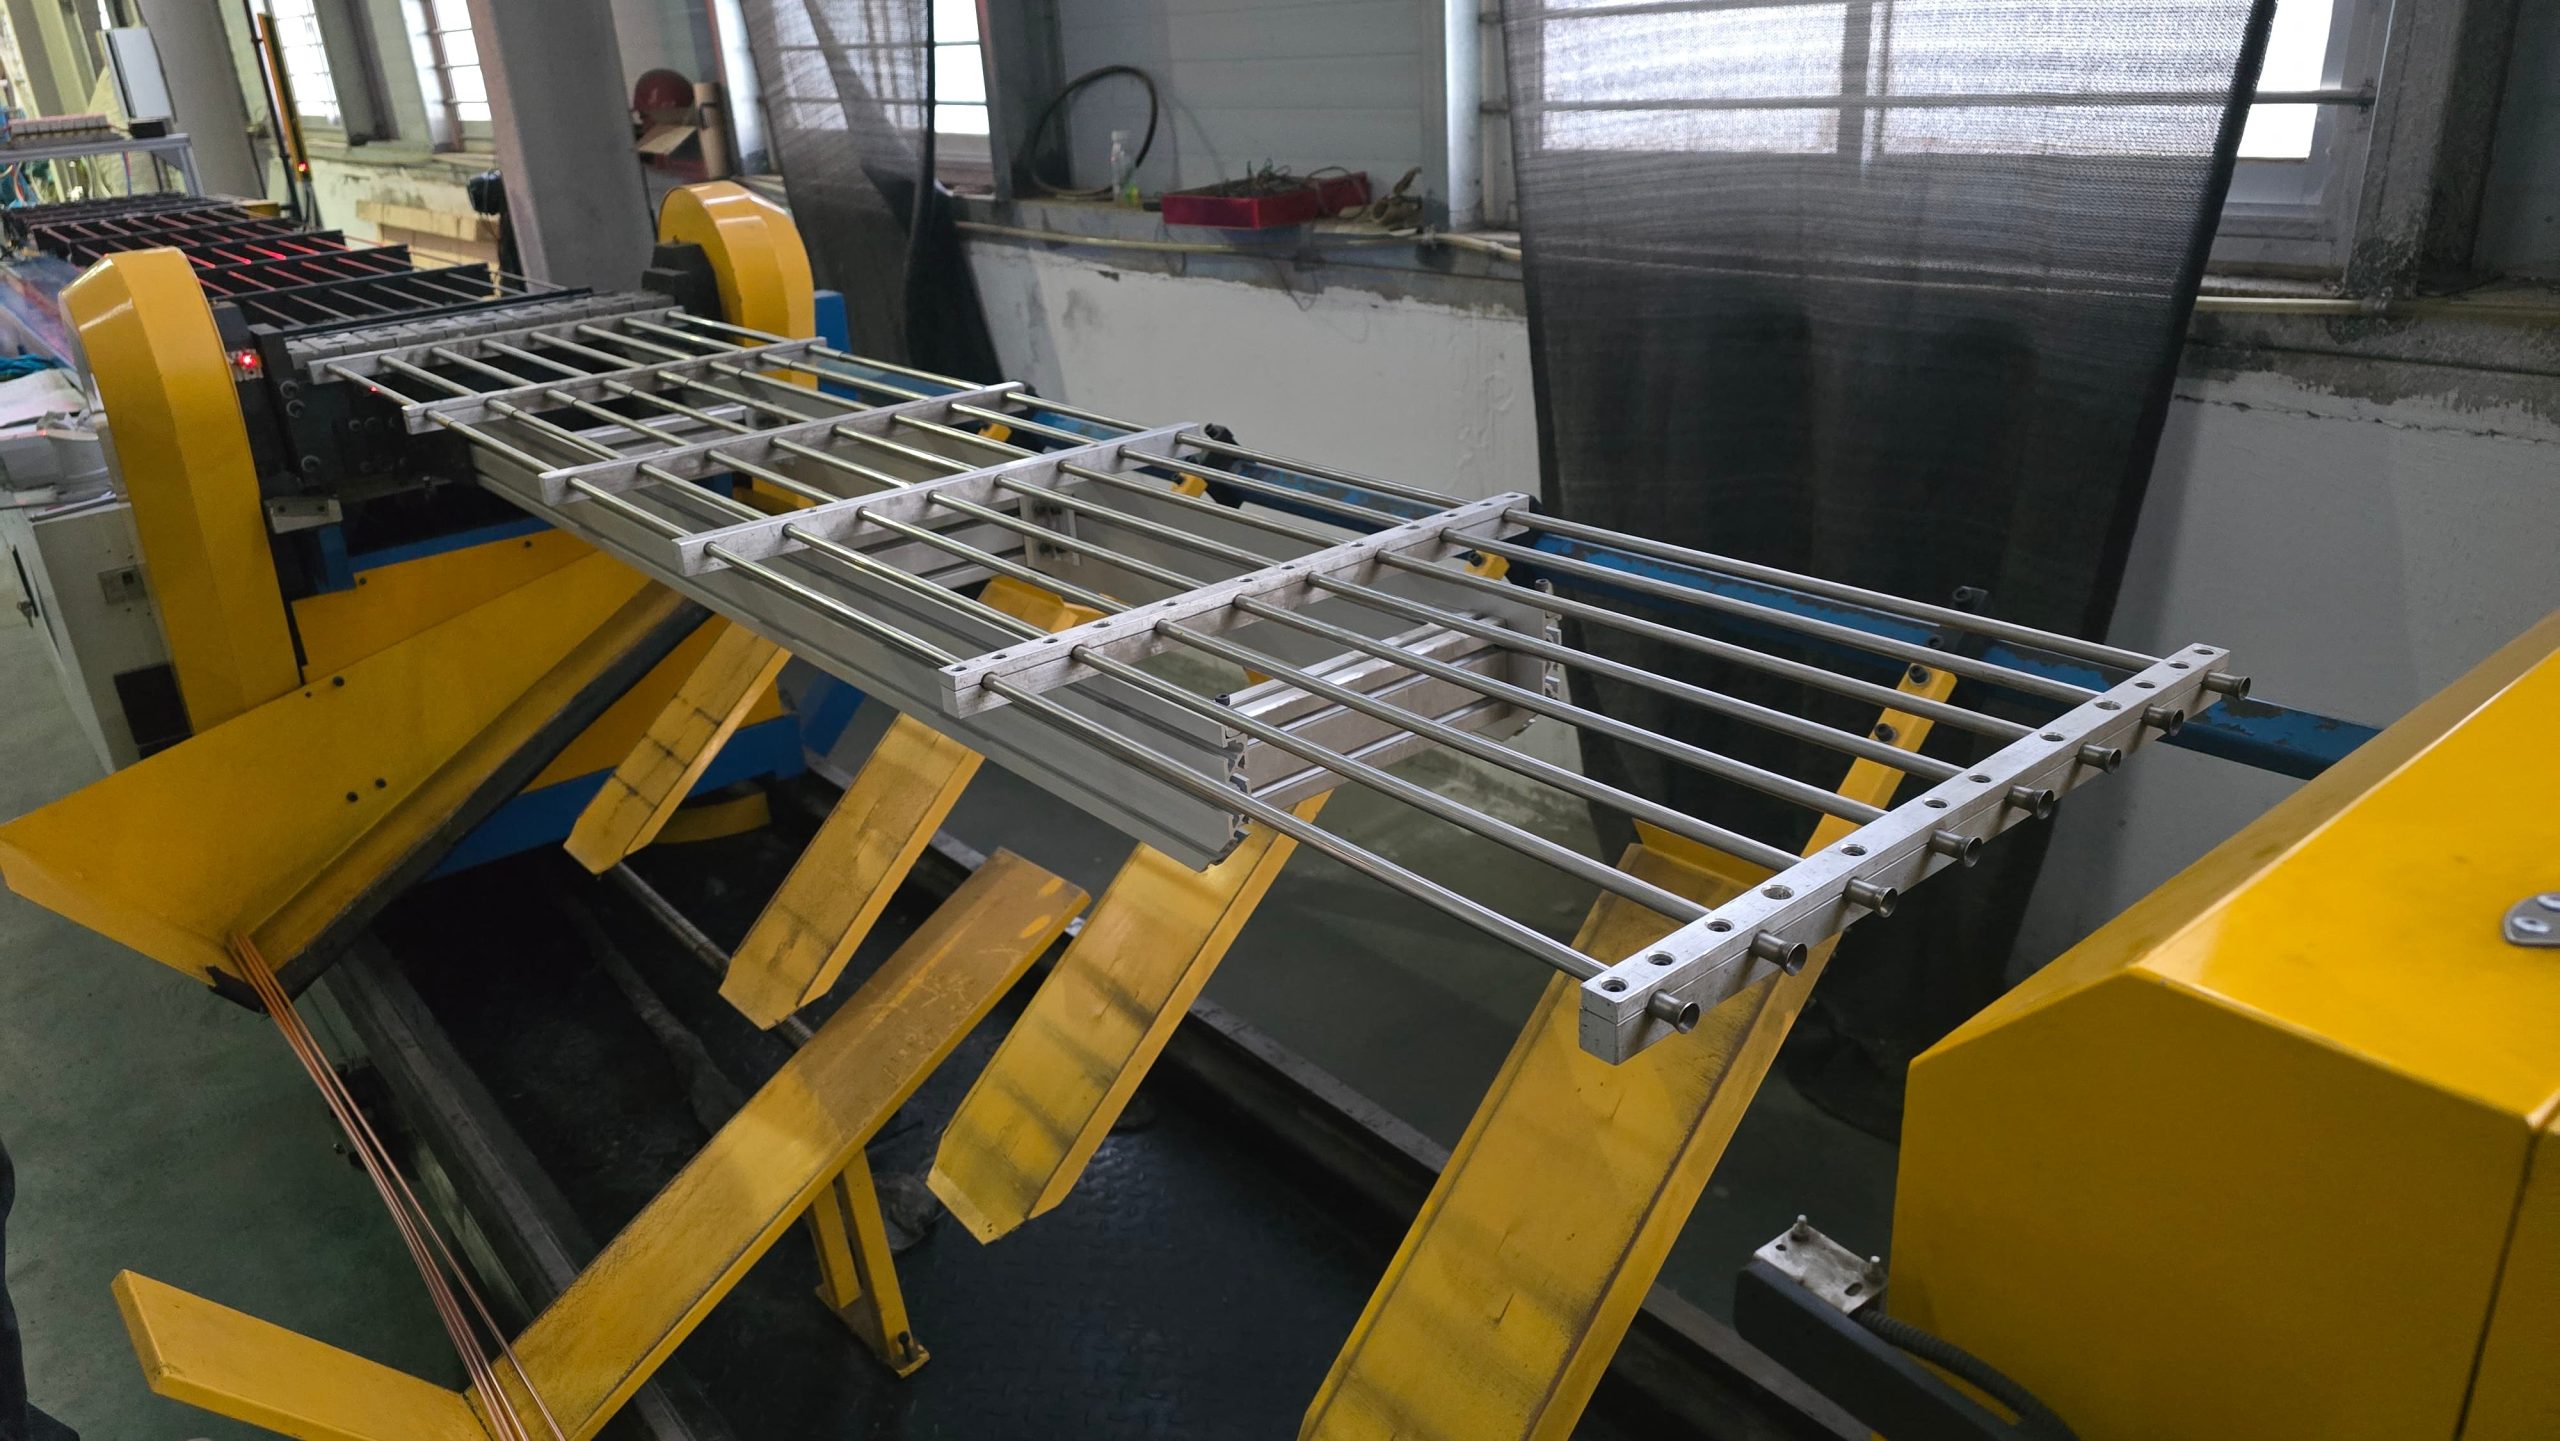
If a factory keeps straightening and cutting separate from bending, long tubes need continuous support, clear locating references and segregated containers. Manual handling without adequate support can introduce friction, slip or small pre-bend deformation before the tube reaches the bending tooling.
Why an Automatic Hairpin Bender Can Add Value
An automatic hairpin bender can connect feeding, straightening, measuring, cutting, bending and unloading that would otherwise take place at separate stations. For stable heat exchanger products, it can eliminate the transport and re-loading of tubes that have already been straightened and cut, while reducing the risk of mixed material as tubes move between operations.
- Reduce transfers and repeated location from the straightening and cutting station to the bending station.
- Link feed, length and bending actions within an approved range of tube diameter, wall thickness and tube length.
- Use recipes, counters and batch identification to provide more consistent data for tube insertion and traceability.
- Reduce repetitive long-tube handling without removing the need for material control, guides, guarding and fault recovery.
Where a Semi Automatic Hairpin Bender Fits
Semi-automatic equipment often creates value where products change frequently, trials are common or demand is not yet stable. It keeps direct control of loading and product confirmation with the operator while making the repeated bending action more consistent than a manual method.
|
When semi-automatic is worth priority |
What to confirm during the enquiry |
|
Tube diameters, lengths, bend shapes or incoming tube forms vary enough to require frequent adjustment. |
Available diameter and length range, rapid adjustment method, guides and long-tube supports, program and parameter handling. |
|
Demand is uncertain or the plant needs space for trials and validation of new coil designs. |
Representative and boundary-product trials, changeover time, first-piece approval and operator responsibilities. |
|
The plant wants to automate one decisive action first and connect loading or logistics later. |
Future loading direction, buffer arrangement, safeguarding interfaces, machine status signals and required data fields. |
Hairpin Quality Problems and Process Adjustments
|
Observed issue |
Likely causes |
Adjustment and optimization direction |
|
Hairpin length drifts or the two legs differ |
Feed slips, length reference is unstable, tube traction varies or unloading pulls on the tube. |
Verify synchronization between feed and cut; validate length and location references with continuous samples from representative material. |
|
Ovality, wrinkling or unstable springback |
Bend tooling, clamping, tube hardness or wall-thickness variation do not match; the parameter window is too narrow. |
Create approved recipes by diameter, wall thickness and bend radius; re-check first pieces after a coil, batch or product change. |
|
Surface scratches or damaged tube ends |
Guides, clamps, storage or unloading contact surfaces are worn; long tubes are not fully supported or are dragged manually. |
Inspect rollers, guides, loading zones and fixtures; add continuous soft support and anti-scratch control for the longest tube. |
|
Unloading creates mixed parts or delays tube insertion |
Unloading direction, stack capacity and downstream takt time were not designed together; buffers do not separate batches or product types. |
Set collection and containers from the tube-insertion rhythm; define batch, orientation and maximum buffer quantity. |
|
One automatic-system fault stops the whole flow |
Feeding, bending, unloading and safety interlocks lack a controlled recovery, bypass or manual procedure. |
Test low material, tube jam, missed pick-up and coil changes during acceptance; assign stop, isolation and restart responsibilities. |
When hairpin quality is unstable, increasing automation is not a substitute for process validation. Tube batch condition, supports, guides, recipes and inspection methods need to be stable first. Otherwise, continuous equipment can accumulate defects and downtime faster than a separated process.

Reviewing a Hairpin Bender With SINOAK
SINOAK can review tube diameter, wall thickness, hairpin length, bend radius, output target, incoming material form, product-change frequency and downstream tube-insertion rhythm to define the boundary of an automatic or semi-automatic hairpin bender. For plants that already use straightening and cutting equipment, the review also considers whether straight-tube loading, long-tube support and hairpin unloading create a new handling bottleneck.
For an initial technical review, share tube and hairpin drawings, target output and factory conditions with SINOAK heat exchanger production equipment and technical support. The proposal should first establish the material route, actual bottlenecks and the process window that can be verified before continuous loading is used to replace intermediate handling.
Information to Prepare Before Requesting a Quote
- Copper tube diameter, wall thickness, material condition, coil or straight-tube supply and expected material-batch variation.
- Hairpin developed length, finished height, bend radius, dimensional tolerance, tube-end requirement and acceptable surface defects.
- Monthly, shift and peak demand for each product family, batch size, changeover frequency and expected growth.
- Actual cycle time, labor time and buffer capacity at straightening, cutting, tube insertion and coil-loading operations.
- Floor clearance, long-workpiece support, material route, electrical and compressed-air services, safety zone and maintenance access.
- First-piece approval, product turning, batch identification, fault recovery, tooling and spare-part maintenance responsibilities.
FAQ
Can an Automatic Hairpin Bender Replace Straightening and Cutting
How Should Semi Automatic Hairpin Bender Capacity Be Calculated
How Can Ovality or Unstable Hairpin Dimensions Be Controlled
Conclusion
Choosing between an automatic and semi-automatic hairpin bender is not a simple comparison of bending speed. An automatic solution is most effective when the route from coil to hairpin is stable, the product family is clear, manual transfer is a real constraint and the factory can support maintenance and fault recovery. When products change often or demand is still being proven, a flexible semi-automatic arrangement can control risk more effectively.
Recent News